...
A reliable plush product development and manufacturing partner For brands Since 2007!

Plush Sewing & Assembly

Engineering every seam for shape, strength, and repeatable character accuracy.

Pufumi transforms approved patterns into stable plush structures through controlled stitching, component alignment, filling preparation, accessory attachment, and assembly sequencing designed for consistent production at scale.

  • 600 sewing machines support flexible multi-SKU production planning.
  • 58+ specialists optimize seams, curves, joints, and silhouettes.
  • 28 core lines accommodate varied sizes and construction complexity.
  • First-piece approval verifies alignment before full-line production begins.
  • Reinforced attachments improve durability around limbs, ears, and accessories.
  • 35+ quality specialists inspect stitching, assembly, shape, and finishing.

Why Sewing Quality Defines the Finished Plush

Correct materials and embroidery cannot compensate for unstable seams, inaccurate component positions or inconsistent assembly. Sewing determines shape, strength, character expression and repeatability across the production run.

Shape and Proportion

Each seam controls part of the finished silhouette. A difference of several millimeters around the face, muzzle, head gusset or body side panel can become visually larger after turning and filling. Stable sewing follows defined notches, seam allowances, curve transitions and alignment points, preventing narrow faces, twisted bodies, uneven limbs or distorted head-to-body proportions.

Component Positioning

Ears, arms, legs, tails, wings and costume pieces must enter the seam at controlled positions and angles. Placement marks alone are insufficient when thick pile hides reference points. Operators also need part direction, insertion depth and assembly order. Incorrect positioning can change the pose, expression, balance or packaging orientation of an otherwise accurate plush design.

Seam Strength

Structural seams contain filling and resist pulling during handling. High-stress areas require suitable thread, controlled stitch length, sufficient seam allowance and local reinforcement. Weak construction may remain hidden before filling, then open under pressure near limbs, hanging loops, weighted inserts or the final closing seam. Inspection therefore starts while the shell remains accessible.

Bulk Consistency

A skilled sample maker can shape one excellent prototype by hand, but commercial production requires repeatable instructions. Released patterns, reference samples, sewing notes, first-article approval and in-process checks translate individual workmanship into a controlled production method. These controls reduce variation between operators, production lines, batches and later replenishment orders.

Plush Programs Requiring Controlled Sewing and Assembly

Different plush formats create different seam, reinforcement and positioning risks. Pufumi adapts the construction plan to product size, intended use, accessories, packaging and target market.

Licensed Character Plush

Character recognition often depends on facial width, eye-to-mouth spacing, hair placement, clothing layers and signature accessories. Sewing instructions identify visual control areas separately from ordinary body seams. Approved front, side and back views guide component placement, while production checks compare the shell and filled unit against the Golden Sample before full-volume output continues.

Collectible Plush Series

Collectible programs may contain several characters, expressions, colorways or rarity levels. Shared body platforms can improve consistency, but every changed face, garment or accessory needs its own released version. SKU codes, bundled panels, accessory kits and line-clearance rules help prevent mixed faces, clothing, cards or packaging during multi-character production.

Plush Keychains

Small dimensions leave less room for seam allowance, turning openings and internal reinforcement. The hanging loop must connect to a load-bearing structure without pulling the head out of shape. Metal rings, lobster clasps or chains also need controlled direction, finish protection and attachment checks before the product enters retail packaging.

Plush Bag Charms

Bag charms move, twist and contact zippers, straps and other hard surfaces during use. Assembly planning considers product weight, hanging orientation, clasp size and internal webbing placement. The attachment point should carry the load without relying only on surface fabric, while the finished charm must remain correctly oriented when suspended from a real bag.

Mascot Plush

Mascots commonly combine large heads, uniforms, logos, hats, shoes or unusual body proportions. Their commercial value comes from recognizable brand details rather than generic softness. Sewing and assembly plans protect the mascot silhouette, color boundaries, garment position and logo orientation while keeping the construction repeatable for annual events and replenishment programs.

Children’s Plush

Products intended for children require early review of seams, filling containment, accessible attachments, cords, hard components and internal parts. Embroidered facial features may replace selected plastic pieces where appropriate. Final requirements depend on the target age, destination market, construction and test plan rather than a universal “child-safe” claim.

From Released Pattern to Sewn Plush Shell

Plush sewing becomes predictable when every production stage receives controlled inputs, creates a defined output and passes a clear inspection point before moving forward.

Pattern Release

Production starts only after the pattern set carries the correct project code, SKU, version, date and release status. Each panel includes grain or pile direction, matching notches, identification marks and seam allowance requirements. Superseded files are removed from the active production area to prevent old shapes from entering cutting or sewing.

Panel Verification

Cut panels are checked for quantity, direction, color, pile orientation and visible defects before sewing. Embroidered, printed and appliqué panels are matched to their correct body sets. Multi-SKU orders use coded bundles so a face panel, body fabric, garment and accessory package remain linked to the same product version.

Component Preparation

Small parts such as ears, tails, wings, horns, hands and footwear may be pre-sewn, turned and locally filled before joining the main shell. Preparation instructions define whether edges require topstitching, whether internal support is needed and which opening must remain accessible for later assembly or shaping.

Main Body Sewing

Body panels are joined in a controlled sequence to maintain access for facial pieces, limbs, internal bags, electronic modules or hidden reinforcement. Operators follow seam maps and workstation references rather than choosing their own construction order. Curved transitions are checked before turning because missed stitches or puckering become harder to repair later.

Structural Assembly

Prepared components enter the main seams at marked positions, depths and directions. Head-to-body connections, limb joints and hanging structures receive additional checks where required. Assembly also confirms symmetry, pose and balance before the shell is fully closed, reducing destructive rework after filling.

Shell Turning

The sewn shell is carefully turned through a planned opening. Narrow limbs, layered garments and long-pile fabrics require suitable opening dimensions and handling methods. Turning should not stretch seam edges, damage embroidery, twist internal parts or pull small components away from their intended positions.

Semi-Finished Inspection

Before filling, inspectors can access seams that will later become hidden. The shell is checked for skipped stitches, open sections, trapped parts, wrong component direction, inconsistent seam allowance and missing reinforcement. Defects are isolated and repaired before filling pressure makes the problem larger or less visible.

Filling Release

Only accepted shells move to filling and shaping. The work order identifies the correct filling material, weight range, internal insert, firmness zones and final opening method. The approved sewn shell therefore becomes a controlled input for the next production stage, not an unverified work-in-progress item.

Pattern Engineering Before Sewing Begins

Reliable sewing starts with a structure designed for cutting, joining, turning, filling and repeat production—not with an operator improvising around a difficult illustration.

Translating Visual Form into Sewable Panels

A flat character drawing does not contain seam lines, panel depth or internal volume. Pattern engineering determines where the design can be divided without damaging its recognizable silhouette. The engineer evaluates the front recognition view, side thickness, back construction, head gussets, muzzle volume, limb shape, tail direction and garment layers.
  • Several engineering decisions are made before the first stitch:
  • Panel division: Each panel must be large enough to cut and sew, yet detailed enough to hold the intended shape.
  • Seam visibility: Highly visible facial areas receive different treatment from hidden underside seams.
  • Pile direction: Fabric direction is marked to avoid mismatched shading and rough handfeel.
  • Turning access: Openings must permit safe turning without becoming visually disruptive.
  • Filling behavior: Curves and gussets are adjusted for expansion after filling.
  • Production handling: Tiny points, narrow channels and excessive panel counts are reviewed for repeatability.
Size changes also require new judgment. A 10 cm mini plush cannot retain every seam and accessory used on a 30 cm retail plush. Small formats often need wider limbs, fewer panels, enlarged facial details and simplified garments. Larger formats may need additional gussets, sectional filling or internal support. The result is a released pattern set that preserves the design while giving cutting, sewing, filling and QC teams an executable structure.

Building a Seam Map and Assembly Sequence

A seam map explains how panels become a three-dimensional shell. It identifies structural seams, decorative seams, reinforcement seams, turning openings and final closing areas. Assembly instructions then define when each ear, limb, tail, garment or internal component joins the product. The sequence matters because later operations can block access to earlier ones. For example, a hanging loop may require internal webbing before the head closes. A sound module may need a controlled cavity and service opening before body assembly. A fixed jacket may need partial attachment while side seams remain open.

  • Key information includes:
  • Joining order: Which panels are sewn first and which remain open.
  • Part orientation: Front, back, left, right, inside and outside directions.
  • Insertion depth: How far an ear, tail or webbing loop enters the seam.
  • Reinforcement location: Where repeated stitching or internal support is required.
  • Inspection gates: Which seams must be checked before becoming inaccessible.
  • Closing method: Where filling occurs and how the opening is finished.

Pufumi’s pattern and sample teams work from the Dongguan core factory, where paper pattern development, sample sewing, modification, PPS and Golden Sample preparation are integrated. Production release occurs after the sample structure, materials and assembly method have been reviewed for repeatability. 

Sewing Methods for Different Plush Materials

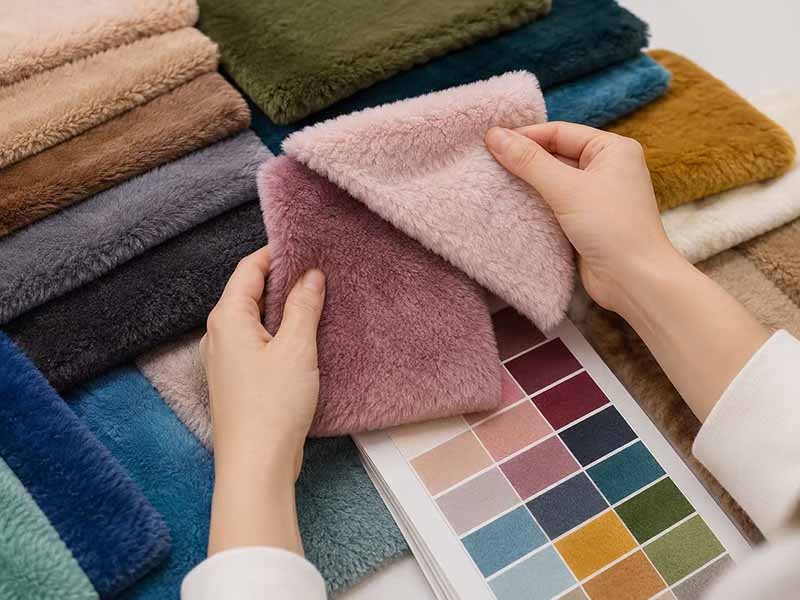
Pile length, stretch, thickness, surface finish and backing construction change how fabric feeds, aligns and closes. Material selection therefore includes a sewing and appearance review.

Short-Pile Plush

Short-pile fabrics reveal seam lines, closing stitches and small surface distortions more clearly than long fur. They work well for crisp character shapes, facial embroidery and compact products, but demand accurate thread color, smooth curves and clean opening placement. Seam allowance and tension are checked carefully because any ridge or indentation remains visible after filling.
  • Clear embroidery performance
  • Strong shape definition
  • High closing-seam visibility

Minky and Stretch Plush

Minky and stretch plush can provide a soft premium handfeel, yet the material may move or grow during sewing. Uncontrolled feeding can change panel length, create wavy edges or shift facial alignment. Pattern dimensions, cutting direction, temporary stabilization and operator handling are reviewed together. Filled dimensions are measured because stretch may alter size even when the flat panels appear correct.
  • Soft surface and flexible form
  • Stretch-sensitive alignment
  • Filled-size verification required

Long-Pile Faux Fur

Long-pile materials can create realistic animals and luxurious textures, but pile may become trapped inside seams or cover small facial details. Operators control pile direction, free trapped fibers after joining and groom the finished seam. Facial zones may use shorter material while the body keeps longer fur, preserving expression clarity without losing the intended tactile effect.
  • Pile-release work after sewing
  • Direction control between panels
  • Selective short-pile facial areas

Felt and Apparel Fabrics

Felt, woven fabrics, knits, satin and coated materials are often used for clothing, appliqués, wings, shoes or props. Their edges, fraying behavior and stretch differ from the main plush fabric. Construction may require folded hems, lining, topstitching, appliqué, interfacing or hidden attachment. Apparel pieces are sampled on the filled body because fit changes with final volume and posture.
  • Edge finishing by material
  • Fit checked on filled samples
  • Attachment recorded in production files

Sample Development Before Bulk Sewing Release

Sampling verifies appearance and proves whether the proposed pattern, seams, assembly order and materials can be repeated under production conditions.

Prototype Development

A prototype begins with artwork review, structure interpretation, material selection, pattern engineering, embroidery preparation, sample sewing, filling and internal evaluation. Standard prototypes normally require 7–12 working days after complete information, sample payment and key materials are ready. Complex characters, layered clothing, special accessories or functional components generally require 12–20 working days.
The first sample primarily answers major questions:

  • Does the silhouette read correctly from the front, side and back?
  • Can the shell be turned and filled without damaging the structure?
  • Are the ears, limbs, tail and garments positioned correctly?
  • Does the selected material hold the intended shape?
  • Are the seams suitable for later production?

Structured Sample Revision

Revision comments must become measurable actions. “Make it cuter” or “improve the expression” cannot guide pattern changes without further definition. Pufumi converts visual feedback into instructions such as moving eyes upward by 3 mm, reducing mouth width, increasing head depth, changing ear angle, narrowing a torso panel or reducing filling in a specific zone.
Each revision record identifies the affected pattern, material, embroidery, assembly or filling operation. The updated sample receives a new version code, preventing earlier instructions from reappearing during later development or production.

PPS and Golden Sample

A production-ready sample uses the intended BOM, released pattern, confirmed embroidery or print files, approved accessories, label position and packaging configuration as far as the project allows. The Golden Sample becomes the physical reference for silhouette, dimensions, workmanship, handfeel, garment fit and assembly position.
Bulk sewing is released only after the responsible approval team confirms the sample and linked production files. A development prototype should not be enlarged directly into production when materials, seams, accessories or packaging remain provisional.

Sewing Specifications for Repeatable Bulk Production

Production teams need measurable requirements and visual references. The specification package connects the approved product with daily sewing, assembly, inspection and corrective action.

Control ItemProduction RequirementMain Risk When UncontrolledVerification Method
Pattern VersionReleased SKU-specific pattern with date and statusOld proportions or incorrect componentsFile-release and workstation check
Seam AllowanceDefined by material, panel and stress levelOpen seams, size variation or distorted shapeFirst-piece measurement
Stitch LengthSelected for fabric backing and seam functionLoose seams, puckering or material damageMachine setup and seam inspection
ThreadConfirmed type, strength and visible colorBreakage, contrast lines or inconsistent appearanceMaterial issue record
Pile DirectionMarked on every directional panelColor shading and rough handfeelCutting and bundle check
Matching MarksNotches and placement points alignedUneven face, limbs or garmentsSewn-shell comparison
ReinforcementMethod and location identifiedLimb, loop or accessory detachmentVisual and directional pull check
Turning OpeningPosition and opening length specifiedDifficult turning or visible closureFirst-shell review
Assembly OrderStep sequence documentedBlocked access, reversed parts or reworkWork instruction audit
Closing SeamMethod, thread and finishing standardVisible ridge, open seam or trapped pileFinal appearance and seam check
Tolerance PointsProduct-specific dimensions and symmetry pointsBatch drift after fillingFirst article and inline measurement
Reference SampleControlled Golden Sample IDPersonal interpretation by operatorsLine-side comparison

Reinforcement for High-Stress Plush Components

Different parts receive different loads during handling, hanging, packing and play. Reinforcement follows the expected direction of force and the internal structure around each attachment.

Arms and Legs

Limbs may be pulled outward, twisted or compressed during use. Reinforcement considers insertion depth, surrounding seam allowance, filling pressure and limb size. Large limbs may distribute force across a wider seam, while narrow limbs need careful curve control and secure joining. Inspection checks both attachment strength and left-to-right position before final filling.
  • Confirm seam capture
  • Check limb direction
  • Inspect after filling

Ears and Tails

Ears and tails are visually sensitive and frequently handled. Narrow attachment bases can concentrate stress, while long tails create leverage during pulling. The pattern may use a wider root, internal seam capture or local reinforcement without creating a hard ridge. Direction, angle and symmetry are inspected together because strength alone does not protect character accuracy.
  • Control insertion depth
  • Match angle references
  • Check root reinforcement

Head Connections

Large-headed characters place substantial load around the neck or head-to-body seam. A narrow connection may stretch, tilt or open after filling and packaging. Construction planning considers head weight, neck circumference, filling distribution and final pose. The connection is inspected before and after filling because internal pressure can reveal weaknesses hidden in the empty shell.
  • Review head weight
  • Inspect full circumference
  • Verify final posture

Hanging Loops

Keychains and bag charms require the loop to connect with an internal load-bearing structure. Sewing only through surface fabric may distort the head or tear the attachment area. Hidden webbing, folded reinforcement or an extended internal anchor can distribute force. The loop direction is tested on the intended clasp and real hanging position.
  • Connect to internal support
  • Check pull direction
  • Confirm hanging orientation

Apparel Attachments

Fixed jackets, capes, shoes and hats may be repeatedly touched or pulled. Attachment points should keep the garment aligned without crushing the body or exposing rough seams. Removable garments require separate evaluation of fasteners and small parts. Workmanship instructions identify fixed, partially fixed and removable areas so operators do not change the intended use.
  • Define fixed areas
  • Protect garment alignment
  • Review accessible parts

Internal Inserts

Weighted bags, sound modules, battery boxes and support pieces must remain contained within defined cavities. Internal bags receive their own seam and closure review before entering the plush shell. The outer construction must prevent migration while maintaining softness, service access and correct weight distribution. Repairs are checked again before the opening is closed.
  • Inspect inner containment
  • Verify internal position
  • Recheck after assembly

Assembly Control for Complex Plush Structures

Complex products require more than joining body panels. Pufumi plans component direction, assembly access, visual alignment, balance and inspection before structures become hidden.

Positioning Three-Dimensional Character Features

Ears, muzzles, horns, wings, tails, hair pieces and footwear create the character’s three-dimensional identity. Each feature has a location, angle, depth and relationship with nearby elements. A technically strong attachment can still be unacceptable when the feature points in the wrong direction or changes the expression.
Assembly instructions combine several references:
  • Pattern marks: Indicate the nominal attachment location.
  • Orientation drawings: Show front, back, inside and outside directions.
  • Insertion depth: Controls exposed length and symmetry.
  • Angle reference: Defines tilt, rotation and resting position.
  • Golden Sample photos: Show the accepted three-dimensional result.
  • First-article measurements: Confirm repeatability on the production line.
Visual zones around the face receive tighter attention because small shifts in the muzzle, ears or hairline can change character recognition. Body features may allow different tolerances depending on size, pile length and pose.
Large heads, backpacks and extended tails also affect balance. Assembly is reviewed in the intended display condition: sitting, standing, lying, packaged or hanging. A bag charm that looks correct on a table may rotate sideways when suspended. A seated plush may tip forward after final filling. The approved assembly method must therefore match real use, not only studio photography.

Planning Access, Sequence and Hidden Construction

Complex structures often fail when assembly order is developed too late. Once a shell is closed, an operator may no longer reach the internal anchor, garment seam or module cavity. Pufumi maps access requirements before production and leaves the correct seams open until internal work is complete.
Typical sequence decisions include:

  • Installing hanging-loop webbing before closing the head.
  • Joining layered ears before the head gusset blocks access.
  • Fixing partially attached clothing while body side seams remain open.
  • Inserting a weighted bag before final torso closure.
  • Locating an electronic module before filling hides the control point.
  • Checking a tail anchor before the back seam becomes inaccessible.

Hidden structures are recorded because they cannot be confirmed from finished-product photographs alone. Work instructions may include internal reference images, section diagrams and inspection sign-offs. Semi-finished inspection verifies reinforcement, internal inserts and seam completion before turning or filling.
A controlled sequence reduces forced handling, unnecessary rework and accidental damage to embroidery or delicate fabrics. It also supports future replenishment because the assembly method remains available even when the original sample operator is no longer assigned to the line.

Protecting Character Fidelity During Sewing

Pattern accuracy must survive cutting, sewing, turning, filling and finishing. Pufumi protects the visual features that make licensed and branded characters immediately recognizable.

Facial Structure

Face shape depends on more than embroidery placement. Forehead curves, side panels, muzzle seams, chin volume and head gussets all change after filling. Sewing checks focus on matching marks, smooth curve transitions and equal panel feeding. The filled first article is compared from the front, profile and three-quarter view before the line continues.
  • Protect eye-to-mouth relationships
  • Control muzzle symmetry
  • Compare filled head depth

Silhouette Control

A character may be recognized first by its ears, hairstyle, head width, body taper or unusual limbs. Seam drift can soften or distort these signature shapes. The production package identifies non-negotiable silhouette points, while first-article checks compare width, height, projection and posture against the approved sample rather than relying only on overall size.
  • Identify signature outlines
  • Measure selected control points
  • Review front and side profiles

Clothing Alignment

Uniforms, capes, collars, belts and shoes must follow the body without covering facial details or pulling the pose out of balance. Garment patterns are fitted on the approved filled body, and attachment marks prevent rotation during production. Logos and stripes are checked in the worn position because flat garment measurements alone cannot confirm final alignment.
  • Fit on filled bodies
  • Control logo orientation
  • Check layered garment edges

Signature Accessories

Hats, bows, horns, backpacks, tools and character props often carry more recognition value than ordinary body details. Their size and angle are recorded through patterns, placement references and sample photographs. Assembly methods balance appearance with durability, packaging space and intended use. Any simplification requires approval before it enters the production file.
  • Preserve recognizable proportions
  • Record accessory angles
  • Approve structural simplifications

Plush Apparel and Soft Accessory Assembly

Character clothing needs independent patterns, materials, edge finishes and attachment instructions. Garments are developed as functional product components rather than decorative additions applied after completion.

Fixed Apparel

Fully fixed clothing stays attached during use and packaging. Sewing may integrate selected garment edges into body seams or secure them after filling at controlled points. The method must prevent rotation, lifted hems and exposed attachment stitches. Fixed apparel is useful when consistent presentation, child-oriented construction or simplified retail handling is the main priority.

Partial Attachment

Partially fixed garments preserve visual depth while limiting movement. A jacket may remain free at the front but attach at shoulders and back. A cape may move along the lower edge while the collar remains controlled. Attachment maps identify every fixed point so production does not accidentally convert the garment into a fully removable or fully rigid structure.

Removable Clothing

Removable clothing supports play, seasonal programs and collectible customization, but introduces fit and accessible-part considerations. Openings, fasteners and small accessories are reviewed against the intended user and market. Garments are tested through dressing and removal cycles, while packaging must prevent loose pieces from becoming lost or mismatched between SKUs.

Hats and Headwear

Hats can be sewn into the head seam, attached at selected points or designed for removal. The decision affects hairstyle construction, ear access, packaging height and final appearance. Structured headwear may need interfacing or internal support, while soft caps require controlled fit so they do not hide the eyes or twist during transport.

Shoes and Footwear

Shoes influence pose, foot shape and standing stability. They may form part of the body structure or fit over a completed foot. Materials, lining, sole stiffness and logo placement are reviewed together. Pair matching is important in multi-SKU production, especially when left and right shapes, colors or printed details differ.

Soft Props

Bags, scarves, fabric tools, wings and other soft props may attach permanently or remain interactive. Construction accounts for scale, filling, edge finish and contact with the main plush surface. Long straps and cords require special review for child-oriented products. Prop versions remain linked to the correct character and packaging set through SKU-coded kits.

Secure Hardware and Functional Part Assembly

Hard components, hanging systems and internal modules require dedicated attachment methods, defined use conditions and inspection beyond ordinary decorative sewing.

Key Rings

Split rings need a fabric or webbing loop sized for the ring diameter and product weight. The loop should remain centered and resist twisting under load. Metal surfaces are checked for sharp edges, plating defects and scratches. Assembly also confirms whether the ring orientation allows the character to face forward when attached.
  • Verify internal anchor
  • Confirm ring movement
  • Inspect metal finish

Lobster Clasps

Lobster clasps suit fashion-oriented bag charms and frequent attachment. Clasp opening, swivel movement, spring return and plating must work with common bag hardware. A swivel improves orientation but adds another connection point. Pufumi checks the clasp, connecting ring, fabric loop and load direction as one attachment system.
  • Test clasp opening
  • Check swivel rotation
  • Match product weight

Ball Chains

Ball chains provide a lightweight option for mini plush and convention merchandise. Chain length, ball diameter and connector quality affect usability. Repeated opening can loosen the connector, so the selected chain must match the product weight and intended handling. The chain is assembled without trapping pile or damaging nearby embroidery.
  • Confirm connector closure
  • Check chain length
  • Review use limits

Plastic Components

Plastic eyes, noses, buttons and decorative parts require compatibility between the component, washer or anchor and surrounding fabric. Attachment is evaluated before filling blocks access. Products intended for young children may require alternative embroidered features or additional risk review. A generic secure-fastener statement cannot replace product-specific testing.
  • Inspect internal locking
  • Check accessible edges
  • Confirm age suitability

Electronic Modules

Sound, light, recording or sensor modules need defined cavities, control locations, speaker paths and battery access. Filling must not press switches or strain wiring. Module installation is verified before final closure, followed by functional testing after filling and packaging. Electronic features may also change labeling, testing and shipping requirements.
  • Control module position
  • Protect wires and switches
  • Test finished function

Weighted Inserts

Weighted pellets or other filling media are contained inside a separate sealed inner bag rather than placed loosely into the outer shell. The inner bag is checked for material, weight, seam condition and closure before insertion. Assembly instructions control its position so weight distribution, posture and handfeel remain consistent across production.
  • Verify inner-bag weight
  • Inspect sealed seams
  • Confirm body position

Closing Seams After Stuffing and Shaping

The final opening must contain filling, preserve the approved silhouette and remain visually discreet. Closing methods depend on fabric, opening position, filling pressure and product use.

Opening Location

The filling opening is planned during pattern engineering, not selected at the filling station. Hidden or low-visibility zones are preferred, but operators still need enough access to turn the shell, insert filling and shape internal areas. An opening that is too short slows production and can stretch the surrounding seam during handling.

Closing Method

Hand ladder stitching, hidden stitching or controlled machine closure may be selected according to product structure. The method defines thread, stitch spacing, seam capture and finishing. High filling pressure or a weighted insert may require additional control. Repair work follows the same approved method rather than an improvised visible over-stitch.

Surface Finishing

Long pile is released from the seam and brushed to restore a continuous surface. Short pile requires careful thread matching and flat closure because the seam remains easier to see. Inspectors check trapped fibers, puckering, exposed thread, indentation and uneven firmness around the opening before the product proceeds to final grooming.

Final Verification

The closed product is inspected under normal handling rather than only while resting on a table. Pressure around the opening should not expose filling or loosen stitches. Shape, dimensions and posture are checked again because closing and final filling adjustment can alter the approved appearance. Repaired pieces receive a separate reinspection before packaging.

First-Article and In-Process Sewing Inspection

Quality is built at production gates where defects remain visible and correctable. Inspection begins with the first sewn shell and continues through assembly, filling, finishing and repair.

Machine Setup Check

Before production begins, needle condition, thread, tension and stitch settings are reviewed against the approved material and seam function. Trial seams reveal puckering, skipped stitches, fabric damage or weak joining before finished panels are consumed. Any machine adjustment is confirmed again after material thickness or seam type changes.

First Sewn Shell

The first completed shell is compared with the released pattern and assembly instructions before filling. Inspectors check panel matching, seam completion, component direction, opening location and reinforcement. Hidden construction can still be reviewed at this stage, making the first shell an essential approval point for complex or high-risk products.

First Filled Unit

Filling pressure exposes dimensional and structural issues that an empty shell cannot show. The first filled unit is reviewed for silhouette, facial expression, firmness, symmetry, balance and closing-seam appearance. Selected measurements are compared with the approved sample before the line receives permission to continue at planned output.

Line Patrol

In-process QC checks active workstations and sampled units during production. Patrol frequency depends on product risk, complexity, production stage and observed defects. Inspectors compare workmanship with the Golden Sample and record recurring issues. Immediate correction prevents a machine setting, assembly error or misunderstood instruction from affecting a large batch.

Changeover Clearance

When production changes between characters, colors, sizes or markets, remaining panels, accessories, labels and documents are removed or counted. The next SKU starts only after the workstation displays the correct sample and files. Changeover clearance is especially important for blind-box series, licensed assortments and products sharing similar body structures.

Rework Control

Defective pieces are identified, isolated and repaired under a recorded method. Rework must not hide a deeper structural problem or mix rejected components into accepted output. After repair, the affected seam, shape, accessory or function is reinspected. Repeated defects trigger investigation of patterns, machine setup, operator method or material condition.

Needle and Foreign Matter

Needle control, broken-needle records, tool management and production-area housekeeping support foreign-matter prevention. Procedures reflect product risk and project requirements. Finished units may receive metal detection where specified. Detection does not replace disciplined needle accountability, because prevention and traceable response remain necessary throughout sewing and finishing.

Final Sewing Audit

Before packaging, the completed unit receives a final workmanship review covering open seams, exposed filling, loose threads, reversed parts, attachment security and visible closure quality. Products are compared with approved samples and SKU references. Packaging begins only after sewing-related defects have been accepted, corrected or formally isolated.

Safety and Compliance Built into Assembly

Target age, destination market and product features influence seam construction, accessible parts, attachments, internal containment and the testing route prepared for each project.

Child-Oriented Structure

Products promoted for children require review of filling containment, accessible hard parts, cords, projections and attachments before sample approval. Embroidery may replace selected hard facial components where appropriate. Seams and internal bags are designed to remain closed through expected handling, while final suitability depends on the specific product classification and test requirements.
  • Confirm target age
  • Review accessible components
  • Plan use-and-abuse testing

United States Programs

US toy and children’s product programs may involve ASTM F963, CPSIA, tracking information, third-party laboratory testing and a Children’s Product Certificate issued by the responsible US manufacturer or importer. Pufumi supports manufacturing samples, BOM information, production records, label execution and testing coordination. Applicable requirements are confirmed by product, age, material and feature set.
  • Prepare representative test samples
  • Maintain production and material data
  • Execute approved tracking information

European Programs

European projects may require product classification, safety assessment, applicable EN 71 testing, technical documentation, conformity procedures and CE-related preparation. Sewing and assembly decisions affect mechanical risks, filling access, small parts and durability. Requirements are mapped to the actual SKU rather than assuming one test report automatically covers every material, size or product version.
  • Confirm applicable EN 71 parts
  • Align sample and production versions
  • Maintain technical file inputs

Functional Products

Weighted, electronic and sensory plush products introduce additional internal components and failure modes. Inner bags, battery access, switches, wiring, module cavities and service openings need controlled assembly. Finished functional checks are performed after filling and packaging where required. Material or module changes trigger a new review because earlier reports may not cover the revised construction.
  • Verify internal containment
  • Test final product function
  • Reassess changed components

Approved Samples Become Production Standards

A physical sample alone cannot guide every department. Pufumi links the approved product to controlled files, inspection references and version records for production and replenishment.

Building the Production File Package

The Production File Package brings the approved design into one executable system. Each file identifies the project, SKU, version, date and release status. Information must remain consistent across patterns, BOMs, embroidery files, packaging documents and QC references.
A sewing and assembly package may include:
  • Approved Sample ID: Links the physical reference to the correct SKU and version.
  • Released Pattern Set: Controls all cut and sewn panels.
  • Seam Map: Identifies structural, decorative, reinforced and closing seams.
  • Measurement Specification: Defines selected finished dimensions and checking methods.
  • BOM: Lists fabrics, thread, filling, accessories, labels and packaging.
  • Embroidery or Print Files: Controls facial features, logos and decoration.
  • Assembly Instructions: Records component direction, insertion depth and sequence.
  • Workmanship Notes: Describes visible standards, pile handling and finishing.
  • QC Checklist: Defines inspection points, risk areas and required records.
  • Packaging Specification: Connects the correct product with labels, cards and cartons.
Production release occurs only when the relevant documents match the approved sample. Later changes enter a formal revision process. Old versions are separated from active files, protecting licensed characters and multi-market products from accidental reuse.
The same package supports replenishment. Teams can compare new materials, samples and first articles with the archived standard rather than rebuilding the product from memory.

Controlling the Golden Sample Lifecycle

A Golden Sample represents the accepted appearance, materials, structure, filling, garment fit and packaging relationship. It must be stored, identified and protected from uncontrolled use.
Pufumi differentiates several physical references:

  • Prototype: Verifies early shape and design direction.
  • Revision Sample: Demonstrates agreed changes.
  • PPS: Reviews production-intended materials and methods.
  • Golden Sample: Becomes the approved production reference.
  • Line Sample: Supports operators and inspectors during production.
  • Retention Sample: Preserves evidence from a completed batch.

The line-side reference should match the formally approved version. Photographs and measurements supplement the sample but do not replace it where tactile or three-dimensional judgment is important.
During repeat orders, the new first article is compared with the Golden Sample and retained production sample. Differences in fabric lot, embroidery, filling, seam position, handfeel or garment fit are reviewed before bulk continuation. When a material becomes unavailable, replacement approval is recorded rather than silently changing the standard.
A traceable Golden Sample system protects long-term consistency, especially for licensed programs, annual mascots, continuing retail SKUs and collections produced in multiple waves.

Sewing Control Across Multi-SKU Collections

Collections require coordinated control of shared structures and SKU-specific details. Coding and line discipline prevent visually similar components from entering the wrong product.

SKU Master List

Every design, size, colorway, expression and packaging version receives a defined SKU record. The list connects product name, dimensions, materials, patterns, embroidery, accessories, approved sample, quantity and production status. Teams work from the same master data rather than separate spreadsheets with conflicting product names or revisions.
  • Assign one code per version
  • Link approval status
  • Track production progress

Panel Bundling

Cut panels remain grouped by SKU, material lot and production batch. Embroidered face panels, body pieces and apparel parts are counted before transfer. Bundle cards identify quantity and next operation. Controlled bundling reduces mixed colors, reversed panels and missing pieces while providing traceability when a sewing defect appears later.
  • Code every bundle
  • Separate material lots
  • Reconcile panel counts

Accessory Kits

Small garments, loops, clasps, labels, cards and internal parts are prepared as controlled kits where appropriate. Kits reduce workstation searching and prevent similar accessories from crossing between characters. Quantity reconciliation identifies missing or surplus components before packaging, where correction would become slower and more disruptive.
  • Pack by SKU
  • Verify kit contents
  • Reconcile unused parts

Workstation References

Each active workstation displays the correct product sample, operation instructions and component orientation. Similar characters require clear visual differences, especially around faces, clothing and hardware. Obsolete samples are removed during changeover. Operators do not select files or accessories only from memory or product nicknames.
  • Display current sample
  • Mark critical differences
  • Remove old references

Changeover Control

Production lines are cleared when moving between SKUs. Remaining panels, thread, accessories, labels and packaging materials are counted or isolated. The new SKU begins after document and sample verification. Controlled changeovers are essential when common body patterns use different expressions, garments or market-specific labels.
  • Clear previous materials
  • Verify next version
  • Approve first changed unit

Packing Reconciliation

Sewing control continues into packaging because a correctly sewn product can still enter the wrong box or assortment. Product codes, cards, barcode data and carton quantities are checked together. Blind-box and retail assortment programs may also require controlled ratios, sealed packaging and documented count reconciliation by carton.
  • Match product and pack
  • Verify assortment counts
  • Record carton contents

Multi-SKU Sewing Program

The following program model shows how sewing risks, sample revisions and production controls can be organized for a commercial character collection.

Program Brief and Engineering Risk

A North American entertainment merchandise program required four 14 cm seated character plush designs, with 600 pieces per SKU and 2,400 pieces in total. Each character shared a common body scale but used different ears, tails, facial embroidery and fixed garments.
The commercial brief included:
  • Four retail SKUs
  • 2,400 total units
  • Three plush fabric types
  • Four character-specific embroidery files
  • Fixed clothing with appliqué logos
  • Internal hanging loops for display
  • Individual polybags and SKU labels
  • One mixed-SKU master carton plan
Early engineering review identified three major risks. First, the narrow neck construction could allow the large heads to lean after filling. Second, the hanging loop entered near the head gusset and could distort the forehead when loaded. Third, two characters used similar body colors and garments, creating a high risk of panel or accessory mixing.
The patterns were separated into shared and SKU-specific components. The neck base was widened, the hanging loop received an extended internal webbing anchor, and character-specific cut bundles were coded before embroidery and sewing. The production plan also required separate garment kits and first-article approval for every SKU rather than approving only the common body.

Sample Revision and File Release

The first sample set was completed in 14 working days after artwork, payment and key material conditions were confirmed. Review found that two ear angles were too upright, one muzzle widened after filling and the garment hem lifted away from the body.
Revision instructions converted visual comments into production actions:
  • Ear insertion marks moved 4 mm outward.
  • Ear rotation changed through a revised seam angle.
  • Muzzle side panels narrowed to control filled width.
  • A hidden garment attachment point was added at each side seam.
  • Filling distribution around the neck was adjusted.
  • Hanging-loop webbing length and position were standardized.
The revised sample set required 9 working days, including pattern updates, new sample sewing, filling and internal review. After approval, each SKU received its own Golden Sample ID, pattern version, embroidery file, BOM, garment reference and assembly sheet.
A pre-production review confirmed materials, color lots, accessory kits, sewing sequence, closing method, label version and carton allocation. Old sample instructions were removed from active files before bulk production began.

Production and Quality Outcome

The representative production schedule allocated 34 calendar days after material readiness and formal production release. Sewing started with a 20-unit first article for each SKU. The first units were checked for head position, ear angle, muzzle width, garment alignment, hanging-loop orientation and closing-seam appearance.
Inline checks were scheduled around early production, midpoint output and pre-completion stages. Panel bundles, garment kits and labels remained separated by SKU. Line clearance was documented during each character changeover. Units requiring sewing repair entered a marked isolation area and returned to inspection after correction.
Before packing, the team reconciled:

  • Accepted finished pieces
  • Rework pieces
  • Rejected pieces
  • Remaining garments
  • Remaining labels
  • Remaining hardware
  • Packed units by SKU
  • Carton quantities

The 2,400-unit program format demonstrates how a collection can share engineering efficiencies without losing character-specific control. Patterns, Golden Samples and retained production references remain available for later replenishment review, subject to material availability and any approved product changes.

Trust, Compliance & Production Assurance

Confidence for global brands and complex plush programs

Pufumi evaluates each project according to its target market, age grade, materials, construction, labeling, and packaging requirements. Depending on the assigned production site and project scope, our team can support ISO 9001 quality-management documentation and coordinate testing to EN71, ASTM F963, CPSIA, REACH, and other applicable standards. Factory audits, certifications, and test reports are verified by issuing body, validity period, facility, and product scope, giving brands greater transparency from sample development through controlled production and delivery.
Frequently Asked Questions

Plush sewing and assembly covers panel preparation, structural stitching, component positioning, reinforcement, turning, internal part installation, semi-finished inspection and final closing after filling. Scope may also include garments, hanging hardware, weighted bags or electronic modules. Embroidery, printing, filling and packaging connect with the process but may be managed as separate production stages.

Yes, subject to engineering review. Pufumi evaluates the front, side and back form, panel division, thickness, pose, garments, accessories and intended size. Details that cannot be repeated reliably in soft materials may require an approved structural interpretation. A prototype is developed before bulk release to confirm appearance and production feasibility.
Standard prototypes generally require 7–12 working days after complete files, sample payment and key materials are ready. Complex characters, multi-layer clothing, unusual materials, weighted structures or electronic features normally require 12–20 working days. Multi-SKU groups and packaging prototypes are scheduled according to the combined development workload.
Seam construction depends on fabric backing, seam location, filling pressure, product size, expected use, target age and attachment load. Pufumi identifies structural and high-stress areas during engineering. Verification may include visual checks, directional pull checks, finished-product handling and third-party testing where required by the market or project specification.
Released patterns contain matching marks and part references. Assembly instructions add orientation, insertion depth and angle information. The first sewn shell and filled first article are compared with the Golden Sample. Line-side visual references and in-process checks help prevent rotation, unequal depth, left-right reversal and position drift during production.
Removable, partially fixed and fully fixed clothing are all possible, depending on design, size, intended user and market. Removable garments need suitable openings and fasteners, while small accessible pieces may affect age grading and testing. Garment patterns, fit, attachment points and packaging are confirmed during sample development.
The hanging loop is normally connected to an internal load-bearing structure rather than only to surface fabric. Webbing length, insertion depth, seam capture and pull direction are defined for the selected ring, clasp or chain. The completed product is checked while hanging in its intended orientation and under relevant handling conditions.
Opening location and closure method are selected during engineering. Depending on material and structure, closure may use ladder stitching, hidden hand stitching or controlled machine sewing. Thread color, stitch spacing, pile release, surface flatness and filling containment are inspected. Repaired closures receive another check before packaging.
Pufumi uses SKU master data, coded panel bundles, separate accessory kits, workstation references, changeover clearance, label verification and packing reconciliation. Every SKU maintains its own approved sample, patterns, BOM and packaging file. Similar characters receive additional visual differentiation at sewing and packing stations.
Pufumi can prepare representative samples, BOM details, production information, labels and supporting documents for project-specific third-party testing. US programs may involve ASTM F963, CPSIA, tracking information and CPC preparation by the responsible US entity. European programs may involve applicable EN 71 testing, technical documentation and CE-related conformity work.

Send Your Sewing Project Brief

Share the information needed to evaluate structure, sample development, sewing methods, quality controls and production scheduling. Helpful files include front, side and back artwork; 3D references; target dimensions; quantity per SKU; intended age; destination markets; material preferences; embroidery or print artwork; garments; hanging hardware; weighted inserts; electronic functions; label requirements; packaging format and required delivery date.

For an existing design, include available patterns, samples, BOMs, inspection standards and photographs of current quality problems. Pufumi can review whether the structure is ready for production, requires a new prototype or needs focused changes around seams, reinforcement, component positions or closing methods.

Licensed and branded projects should include confirmation that the submitting organization owns or is authorized to use the supplied artwork, logos and character assets. Confidential files can enter a controlled review process. Standard prototypes generally require 7–12 working days, while complex structures generally require 12–20 working days after project conditions are complete. Bulk timing is confirmed after sample approval, file release, material readiness, testing scope and packaging requirements are established.

  • Artwork, dimensions and quantity per SKU
  • Target age, market and retail channel
  • Fabrics, garments, hardware and functions
  • Existing sample or quality concerns
  • Packaging and required arrival date
  • Authorization and confidentiality requirements
Start Your Custom Plush Project

Plush Product Development & Manufacturing Support for Global Brands

Share your character artwork, product concept, target size, estimated quantity, destination market, launch timeline, packaging requirements, and any special functions or compliance needs.

Our project team will review your request and recommend a tailored development and manufacturing approach based on character complexity, materials, construction, sample requirements, production planning, packaging, and delivery schedule.

From Character Artwork to Retail-Ready Plush Products

Pufumi supports IP owners, entertainment companies, toy and collectible brands, lifestyle brands, and major retailers with structured plush product development and manufacturing.

Your artwork, unreleased characters, packaging files, target costs, and commercial information are handled as confidential project materials and are not used for other customer projects or public marketing without authorization.

Need Direct Assistance?

Seraphinite AcceleratorOptimized by Seraphinite Accelerator
Turns on site high speed to be attractive for people and search engines.